Home / Capabilities / Site Assessment
OSHA Dust Control Requirements
What OSHA actually requires, what it doesn’t, and where NFPA standards come into enforcement.
The short answer
OSHA Has No Combustible Dust Standard
This surprises people, and a good deal of published guidance gets it wrong. There is no OSHA standard specifically governing combustible dust. What exists instead is a set of general standards, plus the General Duty Clause, plus NFPA standards that OSHA cites as recognised good practice.
Understanding that structure matters, because it changes what compliance actually looks like. You are not demonstrating conformance to a checklist. You are demonstrating that you recognised a hazard and addressed it in a manner consistent with recognised industry practice — which is a different, and in some ways higher, bar.
The framework
How Enforcement Actually Works
STAGE 01
The General Duty Clause
Section 5(a)(1) requires employers to provide a workplace free from recognised hazards likely to cause death or serious harm. Combustible dust is a recognised hazard, so this is the primary enforcement route where no specific standard applies.
STAGE 02
Specific applicable standards
1910.22 (housekeeping), 1910.94 (ventilation), 1910.1200 (hazard communication), and 1910.307 (hazardous locations) all apply to dust-handling operations and are cited directly.
STAGE 03
NFPA as recognised practice
OSHA references NFPA 652/660, 68, and 69 as the recognised industry practice against which the General Duty Clause is assessed. Meeting NFPA is the practical route to defensibility.
STAGE 04
The National Emphasis Program
OSHA’s combustible dust NEP directs targeted inspections at facilities handling combustible materials, which raises the likelihood of scrutiny well above baseline.
In practice
What an Inspection Looks For
A Dust Hazard Analysis
Has the facility identified which materials are combustible, tested them, and documented the analysis? Absence of a DHA is the most common finding.
Housekeeping
Accumulated dust on beams, ledges, and equipment is the secondary explosion risk that turns an incident into a catastrophe. Inspectors look up.
Equipment protection
Venting, isolation, and detection on collectors and conveying equipment, sized against measured explosibility data rather than assumed.
Ignition control
Grounding and bonding continuity, electrical classification, hot work procedures, and control of mechanical ignition sources.
Training
Whether operators understand the hazard, the protection systems, and their own role in housekeeping and response.
Documentation
Design calculations, maintenance records, and inspection logs demonstrating the system is maintained as designed.
Where equipment fits
Design as Part of Compliance
Equipment cannot make you compliant on its own — housekeeping and training are
equally part of the picture. But a collection system designed to NFPA 68/69 with a
documented design basis removes the largest single item from an inspector’s list, and
gives you calculations to produce when asked.
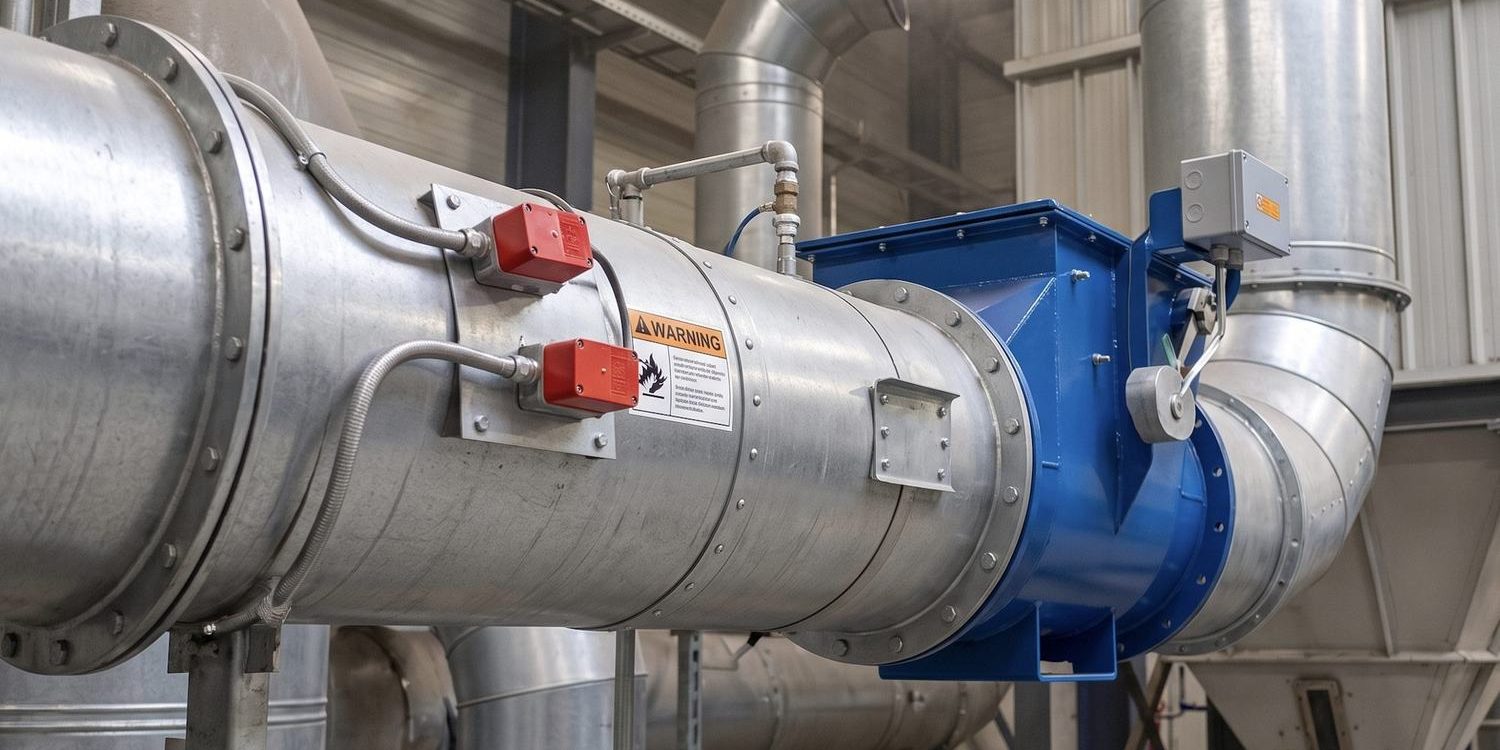
Combustible Dust Collection Systems
Equipment engineered with protection designed in rather than added.
Common questions
FAQs
Is my dust combustible?
Only laboratory testing of your actual material answers this. Material type is a guide, not an answer — the same nominal material from two suppliers can behave differently depending on particle size and moisture.
Do I legally need a Dust Hazard Analysis?
NFPA 652 requires one, and OSHA cites NFPA as recognised practice under the General Duty Clause. In practical enforcement terms, not having one is difficult to defend.
How often should a DHA be reviewed?
NFPA 652 calls for review at least every five years, and sooner if the process, materials, or equipment change materially.
Does OSHA inspect for combustible dust proactively?
Yes, through the National Emphasis Program, which targets facilities handling combustible materials rather than waiting for a complaint or incident.
If I meet NFPA, am I OSHA compliant?
It puts you in a strongly defensible position on the equipment and design side. Housekeeping, training, and ignition control are assessed separately and are where many otherwise well-equipped facilities are cited.
NFPA
Where NFPA Picks Up What OSHA Leaves Open
OSHA enforces through the General Duty Clause and the National Emphasis Program.
NFPA supplies the technical detail those enforcement actions are measured against.
Neither works without the other, and a specification has to satisfy both.
NFPA 652
Fundamentals of Combustible Dust
Establishes the Dust Hazard Analysis requirement and the duty to identify and assess hazards.
NFPA 654
Combustible Particulate Solids
Technical requirements for prevention of fire and dust explosions in processing and handling.
NFPA 68
Deflagration Venting
Sizing and siting of explosion vents, including where the vented discharge is permitted to go.
NFPA 69
Explosion Prevention Systems
Isolation, suppression, and oxidant concentration reduction where venting alone is insufficient.
Following these lets an operator design a system that manages the risk, avoid citations and
shutdowns, and demonstrate due diligence toward employees and neighbouring property.
The documentation matters as much as the hardware: an inspector asks what your DHA
concluded and what you did about it.
Protection strategy
Four Layers, and Why One Is Never Enough
Explosion protection is not a component you add to a collector. It is a set of layers, each covering the failure of the one before it, sized from your own explosibility data.
Deflagration venting sized to NFPA 68 and directed to a safe outdoor location. Where that path does not exist, flameless venting is specified instead.
Isolation — chemical or mechanical valves on the main duct runs, so a deflagration in the collector does not propagate back into the building.
Spark detection and suppression upstream of the collector, catching the ignition source before it reaches accumulated dust.
Grounding and bonding throughout, to control the static that causes a meaningful share of ignitions in the first place.
Each layer is sized from the client’s DHA explosibility data — KSt, Pmax, minimum ignition
energy — not from a general assumption about the material. That is what prevents both over-
engineering and the more expensive error of under-protecting.
A specialty chemical plant handling powders that were corrosive and combustible at once. All four layers specified from the client’s own DHA data, in 316L stainless with smooth internal surfaces and minimal ledges to limit accumulation.
Read the case study →Talk to Someone Who Knows Your Application
Our team has spent their careers on dust collection specifically. Tell us what you’re working on.