Home / Case Studies / Cement Kiln Baghouse
Cement & Aggregates
A 92,000 ACFM Baghouse for a Cement Kiln Running at the Edge of Its Permit
Replacing a twenty-year-old collector on a 2,000 TPD dry-process kiln — engineered for abrasive alkaline dust at sustained 400°F.
The client
2,000 Tons a Day, and a Collector Built for Less
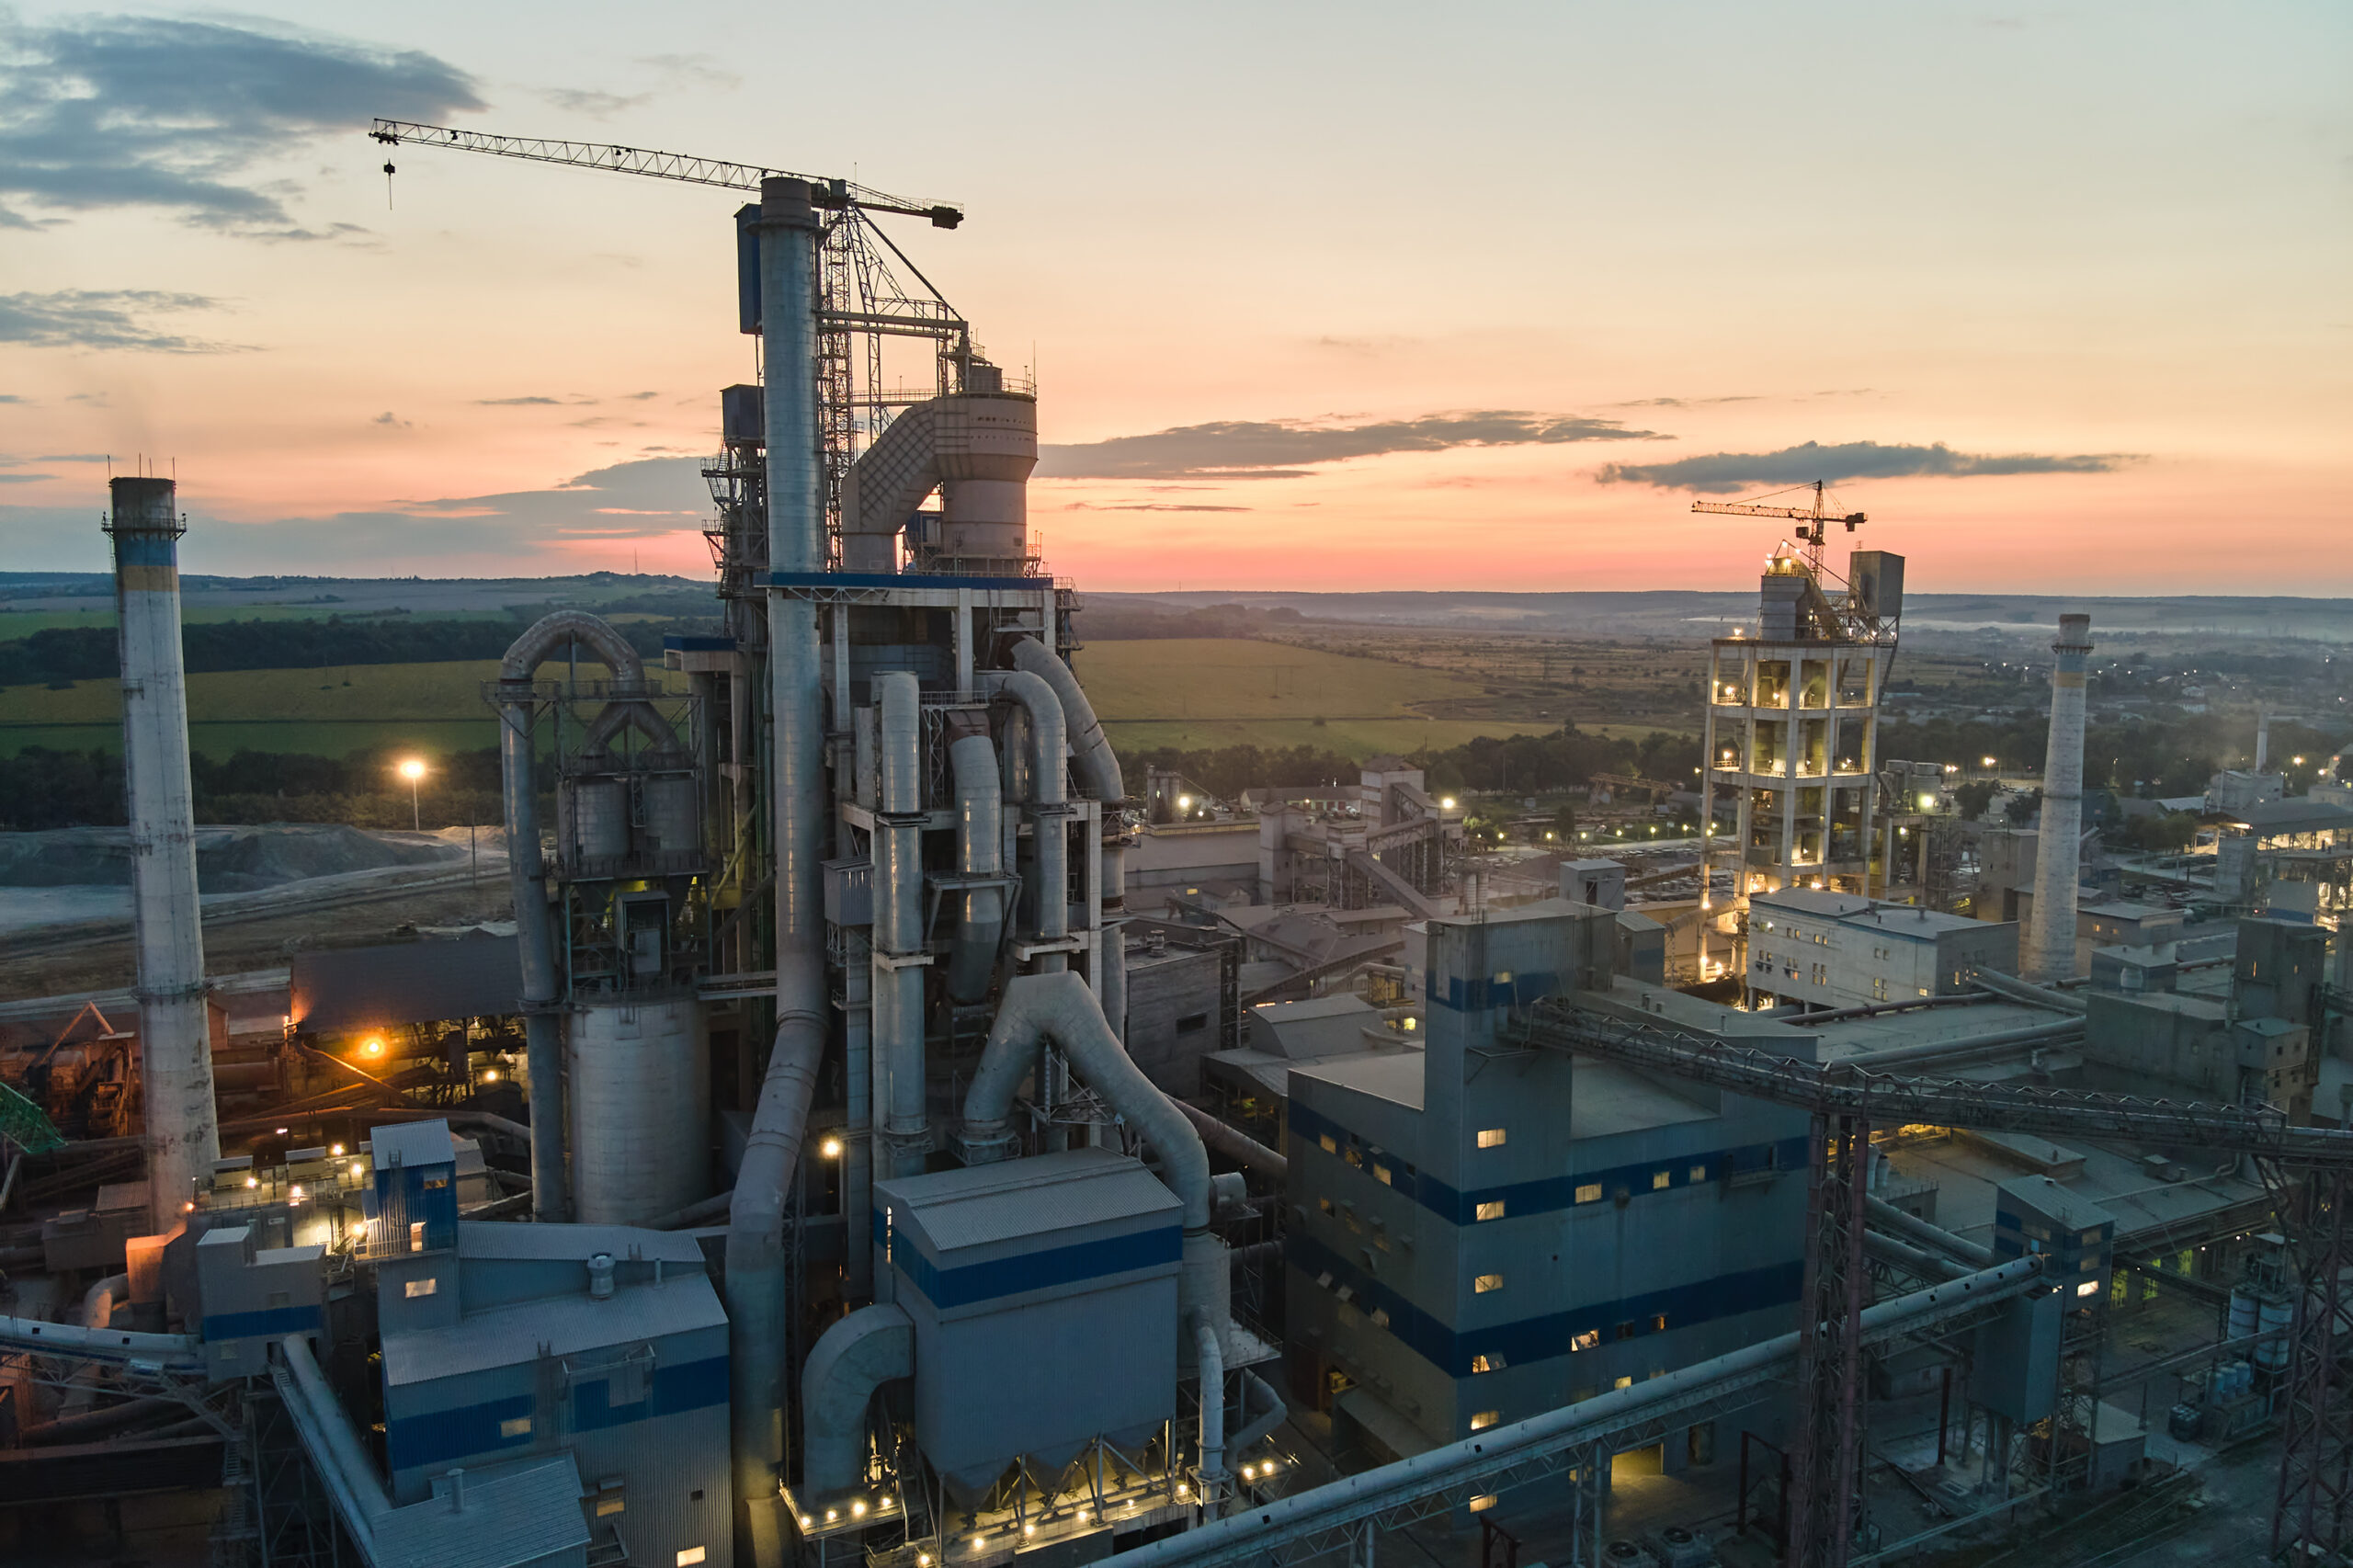
A Midwestern cement manufacturer producing Portland cement on a dry-process rotary kiln rated above 2,000 tons per day.
Kiln operation generates very large volumes of hot, dust-laden exhaust carrying fine particulate, alkaline dust, and trace compounds — a duty where dust collection protects downstream equipment and plant personnel as much as it satisfies the air permit.
The collector serving the kiln line was more than twenty years old and had been modified repeatedly to keep pace with rising production and tightening limits. The engineering and environmental teams concluded that further modification was no longer worth the money.
At a glance
| Industry | Cement production |
|---|---|
| Airflow | 92,000 ACFM |
| Inlet temperature | 350–420°F, spiking on upset |
| Challenge | Abrasive alkaline dust at temperature |
| Solution | Custom pulse jet baghouse |
The challenge
Four Problems, Compounding
Abrasive dust at high loading
Kiln exhaust routinely carried dust concentrations above the old collector’s design limit. The dust — largely calcium compounds and silica — is aggressively abrasive, driving frequent bag failures and a replacement cost the plant could no longer justify.
Emissions margin, and no room in it
The plant was operating close to its permitted limit. When bags began to fail, emissions spiked — and the risk of a notice of violation from the state agency was rising with every cycle.
Sustained high temperature
Inlet temperatures ran between 350°F and 420°F, spiking during upsets. The installed media was never specified for continuous service at that temperature and degraded early, taking filtration efficiency with it.
Maintenance burden
Bag replacement, leak detection, and troubleshooting were consuming maintenance hours the kiln line couldn’t spare, and compressed air consumption for cleaning was running above expectation.
Our approach
Four Decisions That Followed From the Dust
CPE Filter Systems was selected through competitive bid on technical capability, cement experience, and overall value. We began with a site assessment: gas flow measurement, dust sampling and analysis, and review of operating data and permit conditions.
Laboratory analysis confirmed a highly abrasive, moderately alkaline dust with a significant fraction below 10 microns. That combination — fine particulate demanding high efficiency, abrasive particulate demanding gentle handling — drove the design:
- A conservative air-to-cloth ratio of 3.8:1, buying filter life at the cost of a larger collector
- High-temperature fibreglass bags with PTFE membrane, specified for sustained service rather than nominal rating
- Inlet distribution baffles to slow the gas stream and prevent abrasive dust impinging directly on the bags
- Heavy-gauge carbon steel with corrosion allowance and high-temperature insulation
Specifications
As Built
| Airflow capacity | 92,000 ACFM |
|---|---|
| Design temperature | 450°F continuous |
| Filter media | Fibreglass with PTFE membrane |
| Air-to-cloth ratio | 3.8:1 |
| Cleaning system | Low-pressure pulse jet, optimised pulsing |
| Housing construction | Heavy-gauge carbon steel, high-temperature insulation |
| Access | Full walk-in clean air plenum |
| Discharge | Rotary airlock and screw conveyor |
| Safety | Spark detection provisions, access platforms, interlocks |
CPE Filter Systems also supplied the interconnecting ductwork modifications, new dampers, and integration with the plant’s existing control system. The project ran on a fast-track schedule against a planned kiln outage, with our field team working alongside plant maintenance through integration, commissioning, and operator training.
Results
What Changed After Commissioning
Compliance margin restored
The plant now runs consistently below 70% of its permitted emission limit — nearly a third of headroom held in reserve. The notice-of-violation risk that had been building under the old collector is gone, and the margin gives the environmental team a defensible position during regulatory inspection rather than a number to explain.
Maintenance and downtime halved
Maintenance hours committed to the kiln collector, and unplanned downtime attributable to dust collection, are both down 50%. For a kiln line, downtime avoided is production recovered — this is the figure that carried the business case.
Filter life extended by more than half
Bag life has gone from 11 months to 17 months. On a collector this size that is one fewer changeout in every three years, with the associated outage, labour, and media cost removed. The conservative 3.8:1 air-to-cloth ratio is the reason — it costs more in filter area up front and returns it in service life.
Safety and access
The walk-in plenum and improved access platforms have made inspection and maintenance safer as well as faster, which is a meaningful part of where the halved maintenance hours came from.
Related
More From CPE Filter Systems
Service
Site Assessment
Gas flow measurement, dust sampling, and operating review — where every project starts.
Facing Something Similar?
Every one of these started with a site assessment — gas flow measurement, dust sampling, and a look at your operating data. Tell us what you’re dealing with.